Which robotic trends are making the biggest impact on factory automation?
The Robotic Trends That Matter Most in Factory Automation
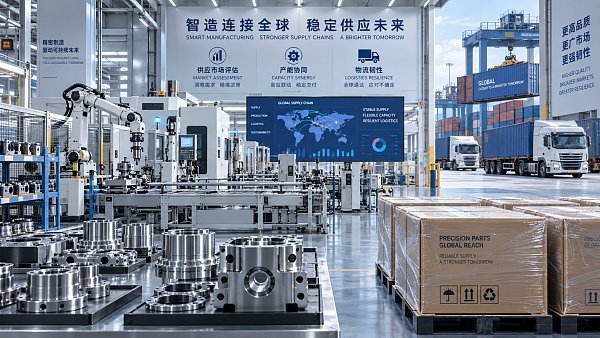
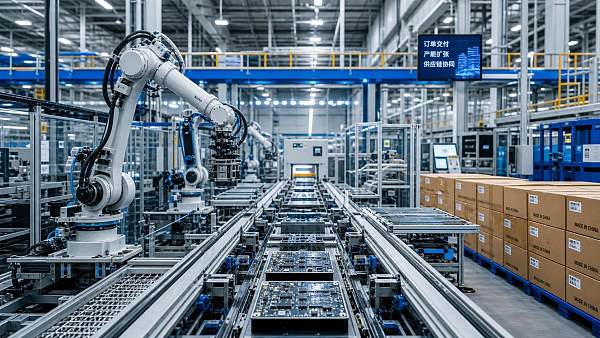
The robotic trends making the biggest impact on factory automation are those that remove constraints across an entire operation, rather than simply speeding up one workstation. Collaborative robots, machine vision, autonomous mobile robots, easier-to-deploy software, and connected data systems are changing how factories handle labor shortages, product variation, quality pressure, and material flow.
For a business decision-maker, the practical question is not whether robotics is becoming more capable. It is which developments can improve output, reliability, and delivery performance in a specific production environment. A robot that performs well in a highly repeatable cell may add little value in a process with unstable inputs, frequent engineering changes, or poorly organized material supply. The strongest automation investments are usually built around a clear operational bottleneck.
Four areas deserve particular attention: flexible automation around people, vision-guided handling and inspection, autonomous internal logistics, and software that makes robotic systems easier to adjust and manage. Their impact comes from improving the factory as a system, not from replacing labor in isolation.
Collaborative Robots Are Expanding Automation Beyond Dedicated Cells
Traditional industrial robots remain essential for high-speed welding, painting, palletizing, heavy lifting, and repetitive assembly. They are often most effective when volumes are high, product geometry is stable, and the task can justify dedicated guarding, fixtures, and engineering work. That model still suits many automotive, metalworking, electronics, and packaging applications.
Collaborative robots, commonly called cobots, have gained attention because they address a different manufacturing problem: how to automate repeatable tasks in environments where product mix changes and human operators still need to work nearby. Their value is often strongest in machine tending, screwdriving, dispensing, light assembly, labeling, testing, and end-of-line handling.
The appeal is not simply that a cobot can operate near people. A useful deployment also requires a safe workflow, appropriate tooling, reliable part presentation, and a task that stays consistent enough for automation. A cobot placed beside an operator does not automatically create flexibility. If parts arrive in random orientations, fixtures are changed frequently, or upstream processes create large variation, the robot may spend too much time waiting for intervention.
Decision-makers should separate “quick installation” from “quick payback.” Many collaborative systems can be physically installed with less infrastructure than a conventional robot cell. The wider project still needs attention to risk assessment, end-effectors, cycle time, operator handoffs, quality checks, maintenance ownership, and restart procedures after faults. A modest project with a well-defined task can produce a more reliable result than an ambitious multi-process cobot deployment designed around vague labor-saving expectations.
Cobots are particularly relevant where labor availability is uncertain, ergonomic strain is high, or production teams need to move experienced operators away from repetitive handling toward inspection, setup, and exception management. They tend to be less compelling where throughput demands exceed the robot’s safe operating speed or where the process already has a highly efficient dedicated automation option.
Machine Vision Is Turning Robots Into More Adaptable Production Tools
Robots are highly repeatable, but they are not inherently perceptive. For many years, this limited automation to carefully fixtured parts and controlled environments. Machine vision changes that equation by allowing systems to locate components, check orientation, identify defects, read codes, verify assembly steps, or respond to changing product positions.
Vision-guided picking is one of the clearest examples. Instead of presenting every component in exactly the same position, a camera system can identify a part’s location and guide the robot toward it. This can reduce the need for some dedicated fixtures and make automation more practical for mixed production. In quality operations, vision can also provide more consistent inspection for defined visual criteria, especially when manual checks are repetitive or difficult to document.
Yet vision should not be treated as a universal substitute for process control. Its performance depends heavily on lighting, contrast, surface condition, part variation, camera placement, and the quality of the decision rules behind it. Reflective metal, transparent packaging, dark surfaces, highly variable raw materials, and changing ambient light can all make a system less reliable than a demonstration suggests.
AI-based vision tools are adding flexibility where rule-based inspection is difficult to configure. They may help classify surface conditions, recognize less predictable objects, or identify patterns that are hard to define with conventional measurements. Their use requires discipline. A model trained on a narrow set of production images may perform poorly when materials, suppliers, finishes, or product variants change. For quality-critical tasks, manufacturers need clear acceptance criteria, controlled training data, traceability, and a process for reviewing uncertain results.
The business case for vision is often stronger when it protects quality and throughput at the same time. A system that confirms part presence, checks orientation before assembly, and records inspection outcomes can reduce rework and prevent errors from moving downstream. By contrast, a vision project focused only on technical novelty can become difficult to support once production conditions drift.
Autonomous Mobile Robots Are Reshaping Material Flow
In many factories, the largest delays do not occur at the robotic workstation. They occur when materials, containers, tools, or finished goods do not arrive at the right place on time. Autonomous mobile robots, or AMRs, are making an impact because they target this internal logistics problem without requiring every transport route to be fixed in the way that conventional conveyor systems often are.
AMRs can support line-side replenishment, work-in-progress movement, warehouse-to-production transfers, finished-goods transport, and returnable-container circulation. Their advantage lies in their ability to navigate a changing facility and to be reassigned as layouts, demand patterns, or shift requirements change. This can be attractive for manufacturers operating mixed-model lines, constrained floor space, or staged expansion plans.
However, internal transport automation succeeds only when the physical and digital flow are both understood. A mobile robot cannot compensate for inaccurate inventory records, poorly defined pickup points, blocked aisles, inconsistent container standards, or unclear ownership of material calls. Congestion is also a risk. Deploying several mobile units in a busy facility may shift the bottleneck from labor availability to traffic management, charging availability, elevator access, or loading and unloading time.
Before selecting an AMR system, factory teams should map the actual movement of materials across shifts, including exceptions. The relevant measure is rarely the distance traveled alone. It is the frequency of moves, the waiting time at each handoff, the reliability of containers, the urgency of delivery, and the cost of a missed replenishment. A short route with unpredictable handoffs may be harder to automate than a longer route with stable, repeatable movements.
AMRs also change the relationship between production planning and logistics. When connected to manufacturing execution, warehouse, or scheduling systems, they can respond to consumption signals and task priorities. The integration effort should be assessed early. A fleet that operates as a standalone transport service may still be useful, but the broader gains depend on whether its tasks are aligned with real production demand.
Robotics Is Becoming More Software-Defined
A major shift in factory automation is occurring in the software layer. Manufacturers increasingly expect robotic systems to be easier to program, faster to reconfigure, and more visible to production and maintenance teams. This includes low-code programming tools, simulation, digital work instructions, remote monitoring, fleet management, and interfaces that connect robots with production data.
The practical effect is not that complex automation no longer requires specialist engineering. High-speed motion, safety design, process integration, and difficult vision applications still demand deep expertise. The change is that routine adjustments can increasingly be handled without rebuilding the full system. For factories with frequent product changeovers, this can be as important as the robot’s mechanical capability.
Simulation and virtual commissioning deserve attention where layouts are complex or disruptions are expensive. They can help teams test reach, collision risks, material paths, cycle assumptions, and line interactions before equipment is installed. Their usefulness depends on whether the virtual model reflects the real process. If actual handling times, operator interventions, or supply variability are omitted, simulation may create confidence without resolving operational uncertainty.
Connected robotics also creates a stronger need for governance. Production leaders need to know who can change programs, how revisions are approved, how downtime is recorded, and how a system can be restored after a fault. IT and operations teams should agree on network segmentation, access controls, software support responsibilities, and data ownership before connected equipment becomes widespread. A factory can lose flexibility if every minor adjustment depends on an external integrator, but it can also create avoidable risk if untrained users can modify critical logic without controls.
The Move From Single Robots to Integrated Automation
The most consequential robotic trend is the increasing integration of robots with inspection, material flow, production data, and human work. A robot arm that loads a machine may improve utilization. That same cell can have a larger effect when it verifies the part, receives the correct production instruction, triggers material replenishment, records exceptions, and routes finished work to the next process.
This does not require every factory to pursue a fully autonomous model. In many operations, a focused automation cell remains the right investment. The point is that robotic projects should be evaluated in relation to upstream and downstream conditions. A bottleneck can simply move if machine loading is automated while quality release, packaging, maintenance, or internal transport remains unstable.
For exporters and manufacturers serving demanding B2B buyers, this broader view can matter beyond labor cost. More consistent process control can support delivery reliability, traceability, documented quality procedures, and the ability to manage product variation. These are often material considerations when buyers assess whether a supplier can support long-term programs or more complex orders.
Where Expectations Often Go Wrong
Robotic trends can create unrealistic expectations when investment decisions begin with equipment rather than process evidence. Several assumptions deserve careful challenge.
- “The robot will solve the labor problem.” It may reduce dependence on manual work for a defined task, but automation also requires technicians, process owners, maintenance capability, and people who can manage exceptions.
- “Flexible automation works for every product mix.” Flexibility has limits. Tool changes, product geometry, packaging variation, part presentation, and cycle-time requirements determine how much variation a system can absorb.
- “A lower purchase price means a lower-cost project.” Integration, tooling, guarding, fixtures, software, training, validation, maintenance, and downtime during installation can outweigh the initial robot price.
- “Vision removes the need for stable inputs.” It can tolerate some variation, but poor lighting, inconsistent materials, and unclear quality standards will still undermine performance.
- “Automation can be evaluated by headcount reduction alone.” The more durable measures include output stability, defect prevention, machine utilization, safety exposure, changeover time, and on-time delivery.
These limits do not weaken the case for robotics. They clarify where value comes from and where additional process work is needed before equipment is installed.
How to Prioritize a Robotic Investment
A useful starting point is to identify the constraint that repeatedly affects production performance. It may be an operator waiting for a machine, a worker performing an ergonomic task, an inconsistent inspection step, frequent shortages at the line, or delays caused by manual movement between processes. The automation opportunity should be specific enough to measure before and after implementation.
Projects should also be assessed across their expected product life. A highly optimized cell may be justified for a stable, long-running program. A modular solution with simpler tooling and faster reconfiguration may be more appropriate when demand is uncertain or product designs change frequently. The right choice is shaped by the production model, not by the newest specification sheet.
What to Watch Next
The next phase of factory robotics will likely be defined less by the arrival of a single breakthrough machine and more by the maturity of connected capabilities. Robots will become easier to deploy in mixed environments, vision will improve the handling of variation, mobile systems will take on a larger role in internal logistics, and software will make automation data more accessible to operations teams.
For decision-makers, the most valuable signal is whether these capabilities reduce a verified operational constraint. The factories that gain the most from robotic trends will be those that treat automation as a production and supply-chain decision: one that links equipment performance with quality, material availability, workforce design, and the ability to deliver consistently when customer requirements change.
 What industrial trade intelligence pricing should include before you subscribeIndustrial trade intelligence pricing explained: compare coverage, data quality, access rights, and workflow value before choosing a subscription that supports smarter trade decisions.
 How an industrial trade intelligence dashboard can identify new supplier marketsDiscover how an industrial trade intelligence dashboard helps identify new supplier markets by comparing capacity, landed cost, logistics resilience, and compliance risk.
 Which global market entry barriers should exporters assess first?Global market entry barriers exporters should assess first: tariffs, compliance, buyer qualification, logistics, and payment risk. Build a practical strategy for confident market entry.
 How trade data aggregation analytics can reveal emerging supplier marketsTrade data aggregation analytics reveals emerging supplier markets by connecting trade flows, capacity signals, logistics, and compliance insights for smarter sourcing decisions.
 When an export market analysis platform can validate demand in a new marketExport market analysis platform insights help validate new-market demand through buyer fit, regulations, logistics, competition, and profitable entry conditions.
 What is driving the beauty and personal care market in the USA?Beauty and personal care in USA is driven by targeted solutions, selective premiumization, digital discovery, clean-label trust, diverse needs, and compliance. Explore key growth opportunities.
 How trade flow monitoring reports reveal changing regional demandTrade flow monitoring reports reveal changing regional demand through import volumes, sourcing shifts, product mix, logistics signals, and regulatory trends. Explore actionable market insights.
 How international market intelligence for investors reduces market-entry riskInternational market intelligence for investors reduces market-entry risk by validating demand, regulations, logistics, and competition before capital is committed.
 How international sourcing intelligence helps identify supplier risk earlyInternational sourcing intelligence helps businesses spot supplier risks early, protect supply continuity, and make smarter global procurement decisions.
 How trade data aggregation analytics reveals emerging supplier marketsTrade data aggregation analytics reveals emerging supplier markets through export trends, input flows, logistics, and regulatory signals. Discover smarter sourcing insights.
 What industrial cluster monitoring in Vietnam reveals about site riskIndustrial cluster monitoring Vietnam reveals hidden site risks across labor, utilities, logistics, compliance, and supplier dependencies. Make smarter sourcing and expansion decisions.
 Food Technology Trends Reshaping Shelf Life, Safety, and Product InnovationFood technology is reshaping shelf life, safety, and innovation. Discover the trends helping food businesses cut risk, improve compliance, and unlock stronger global market growth.
 How electronics manufacturing services are changing with low-volume demandElectronics manufacturing services are evolving fast with low-volume demand. Learn how agile EMS partners improve flexibility, compliance, sourcing resilience, and speed to market.
 How Can Buyers Reduce Procurement Risks for Electronic Components?How to reduce procurement risks for electronic components: learn how buyers assess traceability, lead times, compliance, and supplier types to avoid costly sourcing mistakes.
 What Sourcing Intelligence India Reveals About Supplier Risk and Cost ShiftsSourcing intelligence India reveals hidden supplier risk, compliance gaps, logistics pressure, and real cost shifts—helping buyers compare vendors smarter and source with more confidence.
 Fashion Trends 2026: Which Materials, Colors, and Silhouettes Are Gaining Ground?Fashion trends 2026 spotlight tactile fabrics, mineral colors, and controlled volume. Explore the materials, shades, and silhouettes shaping smarter, more wearable style.
 Smart Device Market Outlook: Key Growth Drivers, Segments, and Business OpportunitiesSmart device market trends are shifting toward system value, industrial demand, and resilient supply chains. Explore key growth drivers, high-potential segments, and business opportunities.
 How Global Trade Intelligence Services Help B2B Firms Evaluate Markets and SuppliersGlobal trade intelligence services help B2B firms compare suppliers, assess market potential, and uncover compliance, logistics, and pricing risks before costly decisions are made.
 Manufacturing Sector Updates for Investors: What Signals Matter Most in 2025?Manufacturing sector updates for investors in 2025: track orders, margins, supply chains, regulation, and exports to spot resilient manufacturers and smarter investment signals.
 How Energy Market Intelligence Helps Businesses Track Price Risks and Demand ShiftsEnergy market intelligence helps businesses spot price risks, demand shifts, and supply pressure early—improving procurement, resilience, and faster strategic decisions.
 Precision Hardware Tools Market: Key Demand Drivers, Segments, and Growth OutlookPrecision hardware tools market trends are reshaping sourcing, compliance, and automation. Explore key demand drivers, segment shifts, regional supply patterns, and growth opportunities.
Global Trade Insights & Industry
Our mission is to empower global exporters and importers with data-driven insights that foster strategic growth.
Search News
Popular Tags
Industry Overview
The global commercial kitchen equipment market is projected to reach $112 billion by 2027. Driven by urbanization, the rise of e-commerce food delivery, and strict hygiene regulations.