How Does Batch Size Affect 3D Printing Cost per Unit?
How Does Batch Size Affect 3D Printing Cost per Unit?
Ordering more parts does not always mean paying less per part. In 3D printing, batch size affects how setup costs, machine time, material consumption, and post-processing are distributed—but savings depend on the printing technology, build utilization, and quality requirements. For procurement teams sourcing printed fixtures, housings, or production components, comparing quotes requires more than a volume discount. Alongside an EMS provider quality certification checklist for electronics manufacturing partners, buyers should assess print consistency, inspection costs, and delivery capacity.
The short answer is that larger batches usually reduce the fixed-cost contribution per part. They do not necessarily reduce the time or material needed to manufacture each part. The strongest savings often come from using available build capacity more effectively; once that capacity is filled, the next quantity increase may trigger another production cycle rather than a better price.
Separate order quantity from build quantity
A purchase order and a printer build are different units of production. One order may fit into a single build, require several builds, or share space with unrelated orders. That distinction explains why supplier pricing rarely follows a smooth downward curve.
Order-level activities include reviewing drawings, checking manufacturability, preparing a quotation, and approving production documentation. Build-level activities include arranging parts, generating supports where needed, preparing the machine, and unloading the completed build. Other activities—such as removing supports or measuring a critical bore—may need to be repeated for every component.
A useful calculation is:
Cost per accepted part = total attributable production and delivery cost ÷ number of accepted parts.
The numerator should include setup, machine operation, consumed material, finishing, inspection, and any applicable packing or logistics costs. The denominator matters just as much: parts that fail acceptance criteria do not provide usable output. Suppliers may account for expected scrap within their prices, so buyers should avoid adding a second scrap allowance without understanding the quotation.
Printing technology changes the volume economics
“3D printing” covers processes with different cost structures. A quantity discount that makes sense for powder-bed production may be unrealistic for filament extrusion, even when both processes can make the same general shape.
Filament extrusion: more parts usually mean more toolpath
In fused filament fabrication, also commonly called FDM, the nozzle deposits material along a toolpath. Adding parts generally adds deposition time, although shared preparation and reduced operator intervention can improve economics. Material consumption also remains closely linked to part geometry, infill, walls, and supports.
For this reason, a full plate does not automatically produce a large unit-cost reduction. A supplier operating several printers can increase throughput, but additional machines still carry operating and ownership costs. Larger orders may benefit from scheduling efficiency rather than a dramatic reduction in physical production effort.
Resin printing: exposure method and height both matter
Laser-based stereolithography traces features, so adding parts can increase scanning time. Projection-based systems expose a larger area at once, making the relationship between quantity and printing time different. Neither process should be priced solely by how many components fit on the platform.
Layer count, recoating or separation steps, supports, washing, and curing all affect cost. Adding similarly sized parts without increasing build height may improve utilization, but washing and support removal still require capacity. For functional components, validated curing conditions and material properties can outweigh a small print-stage saving.
Powder-bed processes: packing helps, within process limits
Polymer powder-bed processes such as SLS and MJF can benefit from arranging parts throughout the available build volume. More productive use of a heating and cooling cycle can reduce its allocated cost per component. However, permitted spacing, thermal behavior, build height, and powder-management requirements limit usable capacity.
Metal powder-bed fusion adds further constraints. Supports, orientation, thermal distortion, stress relief, plate removal, and machining can materially affect the economics. A densely populated plate is not necessarily the lowest-cost plate if it creates difficult finishing operations or inconsistent results.
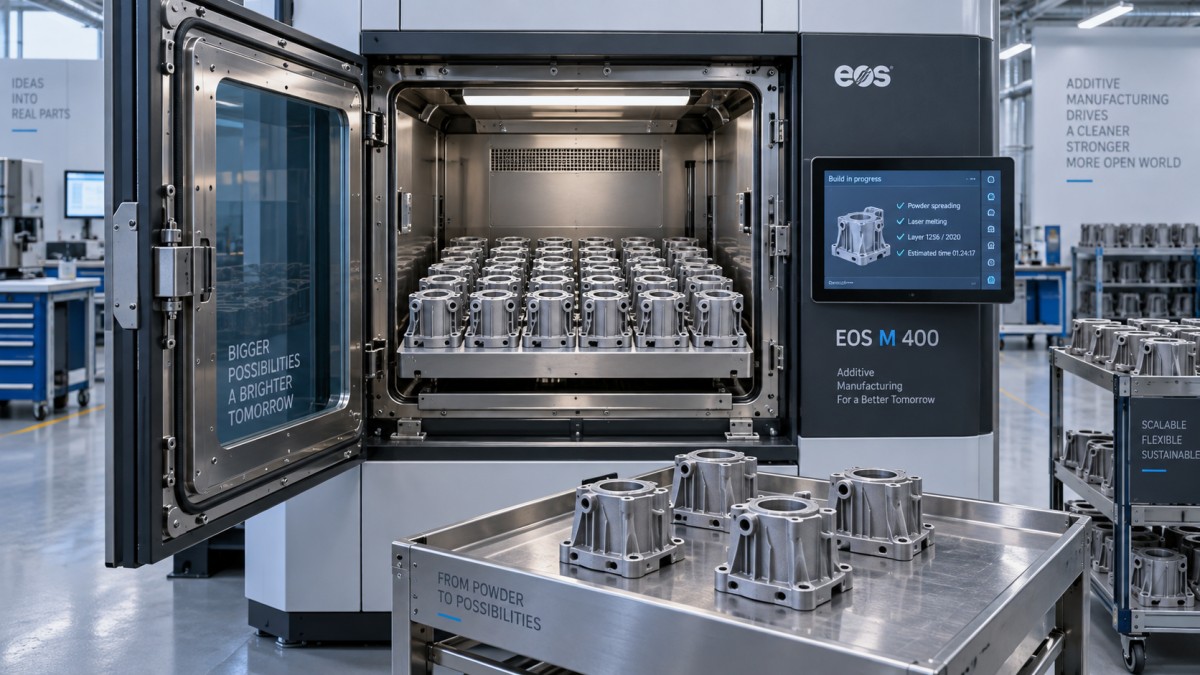
When reviewing a proposed build layout, look beyond occupied space. Ask whether the arrangement preserves required orientation, separation, support access, and inspection access. The objective is productive capacity, not maximum geometric density.
Where savings flatten—or temporarily reverse
Early quantity increases can spread engineering preparation across more components. Later increases may simply repeat an established production cycle. This creates a practical cost floor: material, machine time, finishing, and inspection do not disappear when setup becomes a small part of the total.
Build boundaries can also produce step changes. An order that fits one productive build may have a lower average cost than a slightly larger order requiring an additional, lightly loaded build. A supplier might avoid that penalty by combining work, but shared builds depend on compatible materials, parameters, and delivery schedules.
Do not assume that unused powder becomes waste or that all unused powder is freely reusable. Recovery, refresh ratios, material qualification, and handling practices vary by process and application. Resin and filament also involve losses from supports, purging, cleaning, or failed production. Buyers should ask how material costs are allocated rather than estimating them from finished-part mass alone.
There is also a purchasing distinction: a commercial discount may reflect a supplier’s capacity position, order predictability, or willingness to accept a lower margin. It is not proof that manufacturing cost has fallen by the same amount.
Finishing and quality can become the main cost drivers
A printed housing may leave the machine quickly but still require support removal, surface finishing, threaded inserts, and dimensional checks. A metal component may require heat treatment and machining before it is usable. These operations can dominate the final quote, particularly when tolerances or appearance requirements are demanding.
Larger batches sometimes justify dedicated holding fixtures or more efficient finishing setups. Yet manual work often remains approximately proportional to quantity. If every part needs individual polishing or a documented inspection report, print utilization alone will not create substantial savings.
The acceptance plan should therefore be settled before comparing prices. Specify critical dimensions, measurement methods, surface requirements, and whether testing is sampled or performed on every part. Where destructive testing is required, clarify whether test specimens are included in the ordered quantity or produced separately.
Batch risk deserves attention as well. A failed build can affect several components simultaneously. More parts in one build may reduce allocated setup cost while concentrating schedule exposure. Request the supplier’s approach to replacement production and capacity recovery—not just its expected completion date.
Compare quotes using the same technical baseline
A lower unit price is meaningful only when the deliverable is equivalent. Changing material grade, layer settings, orientation, or finishing can alter both price and performance. For assemblies, those changes may affect fit, fastening strength, sealing, or dimensional stability.
Request quantity breaks around the supplier’s actual build capacity, not only around your usual purchasing tiers. The most revealing questions are:
- Which engineering and setup charges are one-time, and which recur with every build or release?
- How many builds does each quoted quantity require, and is production dedicated or shared?
- Are material, orientation, process settings, finishing, and inspection unchanged across quantities?
- Does the price include accepted quantity, replacement of rejected parts, packaging, and inspection records?
- Will repeat orders use the approved process, and what changes require buyer authorization?
For electronics-related procurement, an EMS provider quality certification checklist can support supplier evaluation, but it does not establish additive-manufacturing capability. Check certificate validity, issuing body, covered site, and scope. A quality-management certificate does not by itself prove that a printed enclosure meets dimensional, flammability, electrical, or environmental requirements.
If an electronics manufacturing services partner subcontracts printed parts, confirm who approves the process, maintains material traceability, controls drawing revisions, and handles nonconforming output. Relevant requirements depend on the application and destination market; they should be verified against project specifications rather than inferred from a general certificate.
Buy for demand and delivery, not just the cheapest unit
An economical production batch can still be an expensive purchasing decision. Buying ahead introduces inventory, storage, cash-flow, and obsolescence costs. This matters for evolving designs, where a revision can make unused housings or fixtures unsuitable before they reach production.
Separate annual demand from release quantity. A forecast or blanket agreement may help a supplier plan capacity, while staged releases reduce inventory exposure. However, smaller releases can reintroduce setup and shipping costs, so the agreement should state what pricing assumes about timing, quantity, and design stability.
For cross-border sourcing, compare landed cost and delivery risk alongside the factory quote. Freight, applicable duties, customs documentation, inspection arrangements, and replacement lead time can change the preferred supplier. A low-price batch that arrives too late to support assembly is not an equivalent offer.
Global Trade Insights & Industry Network (GTIIN) approaches sourcing through this broader trade context: manufacturing capability, procurement trends, regulatory changes, and logistics conditions need to be considered together. That perspective helps buyers distinguish a genuine production saving from a cost shifted into inventory, compliance work, or delivery uncertainty.
Before increasing quantity, ask for a quotation showing the build count, unchanged technical requirements, finishing scope, and delivery assumptions at each price break. Increase the batch where better utilization creates a real saving. Where the cost curve has flattened, preserve purchasing flexibility—or compare another manufacturing route using the same functional and acceptance requirements.
 How to verify sourcing intelligence data before selecting suppliersVerify sourcing intelligence data before choosing suppliers. Learn how to check company records, certifications, and capacity to reduce procurement risk and build a reliable shortlist.
 How to use supplier risk analysis to spot financial warning signsUse supplier risk analysis to spot cash flow pressure, debt risks, and delivery warning signs. Learn practical steps to reduce exposure and protect supply continuity.
 When dual sourcing makes sense in a sourcing strategy for manufacturersSourcing strategy for manufacturers: learn when dual sourcing strengthens supply continuity, reduces disruption risk, and protects production without adding unnecessary complexity.
 How bulk commodities pricing affects long-term supply contractsBulk commodities pricing shapes long-term supply contracts through index rules, freight, quality, volume, and currency risk. Explore strategies for resilient costs and supply security.
 Which global manufacturing trends by sector matter most for sourcing plans?Global manufacturing trends by sector: identify sourcing risks, supplier resilience, compliance demands, and cost drivers to build smarter, more reliable procurement plans.
 What industrial trade intelligence pricing should include before you subscribeIndustrial trade intelligence pricing explained: compare coverage, data quality, access rights, and workflow value before choosing a subscription that supports smarter trade decisions.
 How an industrial trade intelligence dashboard can identify new supplier marketsDiscover how an industrial trade intelligence dashboard helps identify new supplier markets by comparing capacity, landed cost, logistics resilience, and compliance risk.
 Which global market entry barriers should exporters assess first?Global market entry barriers exporters should assess first: tariffs, compliance, buyer qualification, logistics, and payment risk. Build a practical strategy for confident market entry.
 How trade data aggregation analytics can reveal emerging supplier marketsTrade data aggregation analytics reveals emerging supplier markets by connecting trade flows, capacity signals, logistics, and compliance insights for smarter sourcing decisions.
 When an export market analysis platform can validate demand in a new marketExport market analysis platform insights help validate new-market demand through buyer fit, regulations, logistics, competition, and profitable entry conditions.
 What is driving the beauty and personal care market in the USA?Beauty and personal care in USA is driven by targeted solutions, selective premiumization, digital discovery, clean-label trust, diverse needs, and compliance. Explore key growth opportunities.
 How trade flow monitoring reports reveal changing regional demandTrade flow monitoring reports reveal changing regional demand through import volumes, sourcing shifts, product mix, logistics signals, and regulatory trends. Explore actionable market insights.
 How international market intelligence for investors reduces market-entry riskInternational market intelligence for investors reduces market-entry risk by validating demand, regulations, logistics, and competition before capital is committed.
 How international sourcing intelligence helps identify supplier risk earlyInternational sourcing intelligence helps businesses spot supplier risks early, protect supply continuity, and make smarter global procurement decisions.
 How trade data aggregation analytics reveals emerging supplier marketsTrade data aggregation analytics reveals emerging supplier markets through export trends, input flows, logistics, and regulatory signals. Discover smarter sourcing insights.
 What industrial cluster monitoring in Vietnam reveals about site riskIndustrial cluster monitoring Vietnam reveals hidden site risks across labor, utilities, logistics, compliance, and supplier dependencies. Make smarter sourcing and expansion decisions.
 Food Technology Trends Reshaping Shelf Life, Safety, and Product InnovationFood technology is reshaping shelf life, safety, and innovation. Discover the trends helping food businesses cut risk, improve compliance, and unlock stronger global market growth.
 How electronics manufacturing services are changing with low-volume demandElectronics manufacturing services are evolving fast with low-volume demand. Learn how agile EMS partners improve flexibility, compliance, sourcing resilience, and speed to market.
 How Can Buyers Reduce Procurement Risks for Electronic Components?How to reduce procurement risks for electronic components: learn how buyers assess traceability, lead times, compliance, and supplier types to avoid costly sourcing mistakes.
 What Sourcing Intelligence India Reveals About Supplier Risk and Cost ShiftsSourcing intelligence India reveals hidden supplier risk, compliance gaps, logistics pressure, and real cost shifts—helping buyers compare vendors smarter and source with more confidence.
 Fashion Trends 2026: Which Materials, Colors, and Silhouettes Are Gaining Ground?Fashion trends 2026 spotlight tactile fabrics, mineral colors, and controlled volume. Explore the materials, shades, and silhouettes shaping smarter, more wearable style.
Global Trade Insights & Industry
Our mission is to empower global exporters and importers with data-driven insights that foster strategic growth.
Search News
Popular Tags
Industry Overview
The global commercial kitchen equipment market is projected to reach $112 billion by 2027. Driven by urbanization, the rise of e-commerce food delivery, and strict hygiene regulations.