
How to size a concrete block making machine for your daily output
Size a concrete block making machine against the number of acceptable blocks you need each day, not the maximum daily figure in a supplier’s brochure. A machine rated at 10,000 blocks per day may fall short if that figure assumes a different block size, a longer shift, or uninterrupted production.
The capacity decision comes down to a connected set of conditions: blocks per cycle, cycle time, productive hours, expected rejects, and the ability of mixing, handling and curing equipment to keep pace. A useful comparison puts every quotation on the same product and operating basis.
Define the output that must leave the yard
Start with saleable blocks per day: the quantity that must pass the applicable quality requirements and be available for delivery. Use a production target that reflects the planned working schedule and demand commitments, rather than dividing an annual sales forecast by 365 days.
If the requirement is expressed in blocks per month, divide it by the number of production days actually available. Then check whether the resulting daily figure must be achieved every day or whether finished inventory can absorb variation. A machine sized for an occasional peak may be underused for much of the year; a machine sized only for an average may not recover easily after a breakdown or an unusually large order.
Define the product alongside the quantity. A daily target of 8,000 blocks is incomplete without block dimensions, shape and configuration. Hollow blocks, solid blocks and paving products can use different molds, have different numbers of pieces per cycle, and require different cycle times or handling arrangements. If the plant will make more than one product, prepare a separate output calculation for each significant product and allow for mold changes in the production schedule.
Also distinguish freshly molded output from saleable, cured output. A block counted at the machine is not necessarily ready for dispatch: it may still require curing, inspection and handling, and some pieces may be rejected. The machine must produce enough gross units to cover those losses.
Convert daily demand into an hourly machine requirement
The following calculation creates a consistent starting point:
Required gross blocks per day = saleable blocks required per day ÷ (1 − expected reject rate)
Required gross blocks per productive hour = required gross blocks per day ÷ productive hours per day
Productive hours are the hours the machine is expected to cycle, not simply the length of the shift. They exclude planned breaks, cleaning, mold changes and other periods when production stops. If uncertainty remains about short interruptions, apply a separate allowance for them rather than treating the full shift as productive time.
For example, suppose the target is 8,000 saleable blocks per day, with a planning assumption of 3% rejects. If the line has eight scheduled hours and is expected to run for 85% of that time:
- Gross daily requirement: 8,000 ÷ 0.97 = approximately 8,247 blocks.
- Productive time: 8 × 0.85 = 6.8 hours.
- Required machine rate: 8,247 ÷ 6.8 = approximately 1,213 gross blocks per productive hour.
The reject rate and running-time allowance in this example are assumptions, not benchmarks. Replace them with figures supported by the proposed product, process and operating plan. Avoid deducting the same downtime twice: if productive hours already exclude breaks and interruptions, do not apply another utilization percentage for those same losses.
Translate cycle specifications into realistic output
For a machine operating at a constant cycle rate, theoretical hourly output is:
Blocks per cycle × 3,600 ÷ cycle time in seconds
Suppose a proposed mold makes six of the specified blocks per cycle and the complete cycle takes 18 seconds. The theoretical rate is 6 × 3,600 ÷ 18, or 1,200 blocks per hour. At 6.8 productive hours, that produces 8,160 gross blocks. After the assumed 3% rejects, the result is approximately 7,915 saleable blocks per day—slightly below the 8,000-block target.
Although the gap is small, selecting this machine on the example assumptions leaves no room for a slower cycle, additional stops or a higher reject rate. A change in operating hours, mold arrangement or machine capacity would be needed to close it. Conversely, if a supplier can substantiate a shorter complete cycle for the exact product and mix, the calculation should be repeated on that basis.
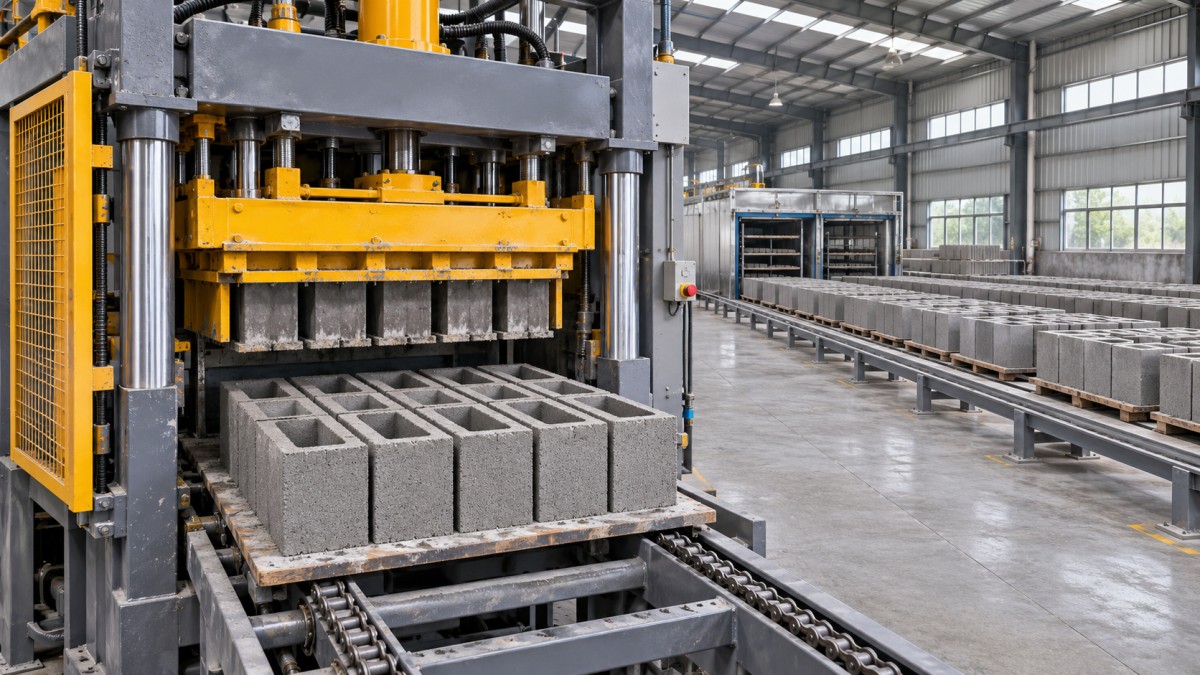
The word complete matters. Ask whether the quoted cycle includes mold filling, vibration and compaction, demolding, and the movements needed before the next cycle begins. A partial machine movement time is not interchangeable with the time between successive batches of blocks leaving the machine.
Cycle time is also product-dependent. A supplier’s fastest figure may not apply to a taller unit, a different concrete mix or a block with a more complex shape. Request the number of pieces per mold and the expected complete cycle time for each product that matters to the daily plan. Where the supplier provides a range, calculate output at both ends rather than relying only on the fastest figure.
Compare quotations on the same production basis
A daily capacity figure has little value unless its assumptions are visible. One supplier may quote output over an eight-hour shift, another over a longer day; one may deduct downtime while another reports theoretical production. The larger number does not necessarily describe the more capable line.
Ask each supplier to complete the same capacity schedule for the proposed block. It should state:
- Block dimensions, type and number of pieces per mold.
- Complete cycle time and the operating conditions used to determine it.
- Shift length, productive hours and any downtime or reject allowances included in daily output.
- Mix characteristics and supporting equipment assumed in the quoted rate.
- Whether the figure represents freshly molded units or acceptable finished units.
Then recalculate each offer using the same shift, utilization and reject assumptions. This separates differences in equipment capability from differences in presentation. It also exposes missing information before a purchase order turns a brochure claim into a contractual dispute.
For a mixed-product schedule, calculate each product’s production time separately. For example, if one product has a theoretical rate of 1,200 blocks per hour and another has a rate of 900, their quantities cannot be added against a single hourly capacity. Divide each required gross quantity by its respective hourly rate, add the resulting run times, and then add mold-change and other planned stoppage time. The total must fit within the scheduled shift, with an appropriate allowance for interruptions.
Check the capacity of the whole line
The block machine can only sustain its calculated rate if material arrives and newly molded products are removed at the same pace. A quoted machine capacity is therefore not the same as the capacity of a complete production line.
Mixing and material supply. The mixer must deliver the required volume of usable concrete at the machine’s consumption rate. Compare mixer output using the supplier’s stated batch size and complete batch cycle, including loading, mixing and discharge. A nominal mixer volume alone does not establish hourly supply. Cement, aggregates, water and any additives also need to be available and dosed consistently; waiting for a batch directly reduces productive machine time.
Pallets and handling. Fresh blocks require suitable support and timely transfer away from the machine. Check the capacity of conveyors, elevators, racks, forklifts or manual handling arrangements included in the line. The pallet count must cover pallets at the machine, in transfer, occupied during curing and returning for reuse, with a practical allowance for the operating cycle. A shortage can stop an otherwise capable machine.
Curing and yard space. Daily output must fit through the planned curing process and into the available storage and movement area. Estimate space and rack requirements from the number of blocks produced per day, their arrangement, and the time they occupy the curing and storage system. That occupancy time depends on the product and process; it should not be assumed from the machine’s cycle time. Access routes and handling space matter as well as the footprint occupied by blocks.
Labor and utilities. Confirm the staffing assumed in the supplier’s output calculation and whether those people are available for mixing, machine operation, transfer and stacking. Review the electrical supply and other utility requirements for the complete line, not just the block press. A machine that can cycle at the desired rate under one staffing or utility arrangement may not do so under another.
Decide how much capacity margin is justified
A margin is useful when demand is uneven, recovery time after a stoppage is limited, or key assumptions are uncertain. It is not a substitute for a credible production calculation. If the target already uses conservative productive hours and an allowance for rejects, adding a large percentage on top without explaining the risk being covered can lead to unnecessary investment.
Test a small number of relevant scenarios: normal production, a slower cycle for a difficult product, and a day with less available running time. The comparison should show whether the proposed line can meet the required delivery schedule, whether finished inventory could cover a shortfall, or whether an additional shift is a practical alternative to a larger machine.
More nominal capacity can also create downstream costs. A faster press may require a larger mixer, more pallets, additional curing space or higher handling capacity before its extra output is usable. Compare the cost of the complete configurations, including molds, installation, spare parts and the supporting equipment needed to reach the specified output.
Put the capacity claim into acceptance terms
Before ordering, agree on a written capacity basis tied to the product the line is being purchased to make. Define block dimensions, mold configuration, mix conditions, shift duration, cycle-time measurement and the supporting equipment included. State whether the acceptance figure is gross machine output or acceptable finished output, and specify how quality will be assessed against the applicable product requirements.
A witness run or acceptance test should use representative materials and operating conditions where practicable. A short demonstration can confirm that the machine cycles and produces the specified mold count, but it does not by itself establish sustained daily output, curing capacity or long-term reject rates. The test scope should make those limits clear, along with the procedure for addressing a result that falls short.
The right size is the smallest complete line that can meet the required saleable output under agreed, credible conditions—with enough capacity to manage the interruptions and product changes that the production plan actually anticipates. The calculation is straightforward; the purchasing discipline lies in making every supplier use the same assumptions.
 U.S. Trade Deficit Narrows to $105 Billion in September 2026U.S. trade deficit narrowed to $105 billion in September 2026 as exports rose 1.9%. Explore what the latest figures reveal about trade flows.
 How to verify international trade intelligence updatesVerify international trade intelligence updates with practical checks for sources, regulations, trade data, and disruptions. Turn complex claims into reliable insights.
 How investors can assess cyclicality in the manufacturing industryManufacturing industry analysis for investors: learn to assess cyclical demand, cash flow and downside risks to make more informed investment decisions.
 US ISM Manufacturing PMI Rises to 55.5% in October, Beating ForecastsUS ISM Manufacturing PMI rose to 55.5% in October 2026, beating forecasts. Explore what stronger orders and production could mean for manufacturers.
 China Manufacturing PMI Falls to 49.3 in OctoberChina manufacturing PMI fell to 49.3 in October, signaling renewed contraction. Explore the role of weak export orders and domestic demand.
 Can you trust flexible packaging market intelligence forecasts?Can you trust flexible packaging market intelligence forecasts? Learn how to verify sources, challenge assumptions, and assess demand before making costly investment or sourcing decisions.
 When is supply chain disruption management consulting worth the cost?When is supply chain disruption management consulting worth the cost? Learn how to compare fees, avoidable losses, and recovery options to make a confident investment decision.
 How to use macroeconomic analysis to forecast industrial demandApply an industrial macro analysis methodology to forecast demand, interpret economic signals, and plan inventory and capacity. Discover practical steps for smarter business decisions.
 How to assess Singapore suppliers with global supply chain intelligenceExplore international supply chain intelligence Singapore buyers can use to verify suppliers, assess capabilities and delivery risks, and make confident sourcing decisions.
 Which macroeconomic indicators help forecast U.S. industrial demand?Explore industrial macro analysis USA decision-makers can use to forecast demand. Track new orders, inventories, and credit signals to sharpen procurement and capacity decisions.
 Can a food processing manufacturer meet your small-batch needs?Can a food processing manufacturer meet your small-batch needs? Discover how to assess minimum orders, costs, packaging, and safety to choose the right partner for your launch.
 How to verify sourcing intelligence data before selecting suppliersVerify sourcing intelligence data before choosing suppliers. Learn how to check company records, certifications, and capacity to reduce procurement risk and build a reliable shortlist.
 How to use supplier risk analysis to spot financial warning signsUse supplier risk analysis to spot cash flow pressure, debt risks, and delivery warning signs. Learn practical steps to reduce exposure and protect supply continuity.
 When dual sourcing makes sense in a sourcing strategy for manufacturersSourcing strategy for manufacturers: learn when dual sourcing strengthens supply continuity, reduces disruption risk, and protects production without adding unnecessary complexity.
 How bulk commodities pricing affects long-term supply contractsBulk commodities pricing shapes long-term supply contracts through index rules, freight, quality, volume, and currency risk. Explore strategies for resilient costs and supply security.
 Which global manufacturing trends by sector matter most for sourcing plans?Global manufacturing trends by sector: identify sourcing risks, supplier resilience, compliance demands, and cost drivers to build smarter, more reliable procurement plans.
 What industrial trade intelligence pricing should include before you subscribeIndustrial trade intelligence pricing explained: compare coverage, data quality, access rights, and workflow value before choosing a subscription that supports smarter trade decisions.
 How an industrial trade intelligence dashboard can identify new supplier marketsDiscover how an industrial trade intelligence dashboard helps identify new supplier markets by comparing capacity, landed cost, logistics resilience, and compliance risk.
 Which global market entry barriers should exporters assess first?Global market entry barriers exporters should assess first: tariffs, compliance, buyer qualification, logistics, and payment risk. Build a practical strategy for confident market entry.
 How trade data aggregation analytics can reveal emerging supplier marketsTrade data aggregation analytics reveals emerging supplier markets by connecting trade flows, capacity signals, logistics, and compliance insights for smarter sourcing decisions.
 When an export market analysis platform can validate demand in a new marketExport market analysis platform insights help validate new-market demand through buyer fit, regulations, logistics, competition, and profitable entry conditions.


Global Trade Insights & Industry
Our mission is to empower global exporters and importers with data-driven insights that foster strategic growth.
Search News
Popular Tags
Industry Overview
The global commercial kitchen equipment market is projected to reach $112 billion by 2027. Driven by urbanization, the rise of e-commerce food delivery, and strict hygiene regulations.