How to match industrial automation systems to packaging line speeds
How to match industrial automation systems to packaging line speeds
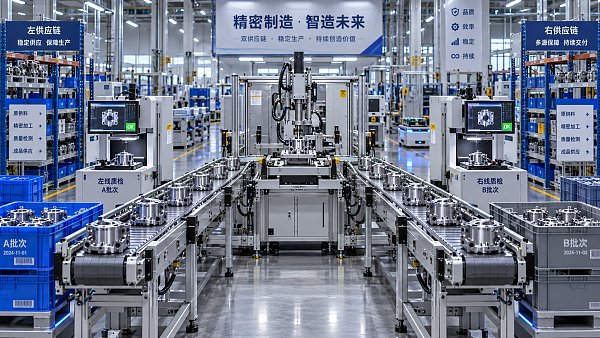
Matching industrial automation systems to packaging line speeds requires more than comparing rated throughput. The real challenge is aligning machine cycle times, conveyor synchronization, sensor response, and control latency with actual production conditions. Equipment that performs well at nominal speed may struggle during product changeovers, upstream interruptions, or restart sequences.
For technical evaluation, the useful question is not “How fast can this machine run?” It is “Can this combination of equipment deliver the required number of acceptable packs, across our product range, without creating unstable transfers or excessive downtime?” That distinction changes how you specify controls, assess robotics, and compare supplier proposals.
Define the output requirement before choosing hardware
Start with required good output over a defined production period. Separate this from instantaneous machine speed. A packaging line may reach its advertised rate while running, yet miss the shift target because of replenishment stops, rejects, cleaning, or lengthy format changes.
Keep the units consistent. Filling may be measured in containers per minute, wrapping in packs per minute, and case packing in cases per minute. Convert every station to a common product-equivalent rate, accounting for pack quantities and parallel lanes. Otherwise, apparently compatible machines can have substantially different capacities.
Two relationships help establish the initial requirement:
- Required average good output: acceptable units required divided by the defined production window.
- Nominal capacity estimate: required average good output divided by the expected combined availability, performance, and quality factor.
The second relationship is a planning estimate, not a guarantee. Use measured production losses where possible, and define whether planned changeovers are inside or outside the time window. Do not count the same loss twice. If no operating history exists, document the assumptions and test how the capacity requirement changes when they worsen.
Specify a speed envelope for each important format: minimum stable speed, normal production speed, and short-duration recovery speed. Include product dimensions, weight, packaging material, orientation, and changeover frequency. A supplier’s highest-speed format should not become the acceptance criterion for your entire product mix.
Translate line speed into a station-level timing budget
For a single-lane station handling one unit per cycle, the available cycle time in seconds is 60 divided by units per minute. As an illustrative calculation, 120 units per minute gives a 0.5-second interval between units. This is not necessarily 0.5 seconds of usable motion time: feeding, settling, gripping, processing, and release must fit the actual sequence.
Batch and continuous-motion machines need different treatment. A multi-head machine may process several products per cycle, while a rotary system overlaps operations across multiple positions. Ask suppliers to explain what their quoted “cycle time” includes and how it translates into sustained output.
Map the process from infeed to palletizing. At each station, identify the physical constraint: sealing dwell, fill settling, label placement, inspection exposure, robot travel, or case formation. Automation can reduce waiting and improve coordination, but it cannot remove a packaging process requirement simply by issuing commands faster.
The bottleneck may also change by format. A lightweight pack might be limited by handling stability, while a larger pack reaches a sealing or robot payload limit. Compare station capacities by representative product family rather than accepting one line-wide maximum speed.
Evaluate the complete control path, not just PLC scan time
A fast PLC does not automatically produce accurate high-speed packaging. The relevant delay runs from product detection through input processing, controller execution, network transmission, output updates, and actuator response. Timing variation matters too: consistent delay can sometimes be compensated, whereas unpredictable jitter makes positioning less reliable.
For moving products, convert delay into distance. At an illustrative conveyor speed of 1 metre per second, 10 milliseconds corresponds to 10 millimetres of travel. Whether that is acceptable depends on the registration tolerance and the available correction method. This is why encoder-based tracking or hardware position capture may be needed even when ordinary PLC logic handles the broader machine sequence.
Request timing information under the proposed configuration: active axes, remote I/O, inspection traffic, data logging, and operator-interface communication. A lightly loaded demonstration controller is not equivalent to the delivered system.
The architecture should follow the task rather than a preference for one technology:
For servo sizing, examine reflected inertia, peak and continuous torque, acceleration, thermal duty, and mechanical stiffness. For robots, assess the complete pick-and-place sequence, including gripping confirmation and product release. Neither unloaded axis speed nor a short laboratory robot cycle establishes usable packaging capacity.
Synchronize product flow and give interruptions somewhere to go
Matching conveyor speeds is not the same as matching throughput. Capacity depends on product pitch as well as belt velocity. Transfer gaps, slipping packs, inconsistent spacing, and accumulation pressure can upset an otherwise adequate design.
Define which device provides the motion reference and how other axes follow it. Registered processes may require electronic gearing or camming; loosely coupled machines may work better with independent speed control and accumulation. The correct choice depends on whether products must maintain a precise position relationship or can safely queue between operations.
Buffer capacity should come from interruption behavior. If upstream production continues during a downstream stop, the initial accumulation requirement is incoming units per second multiplied by the intended bridging time. Convert that quantity into usable conveyor length or storage positions, allowing for existing occupancy and product spacing.
A buffer also needs a recovery plan. If downstream equipment resumes only at the upstream production rate, the accumulated stock will not clear while upstream continues running. Provide justified recovery capacity, controlled upstream slowdown, or another operating strategy. Excess accumulation is not harmless: fragile products, open containers, and temperature-sensitive goods may impose strict limits.
Specify machine-to-machine behavior for blocked, starved, stopping, and restarting conditions. Include what happens to partly processed packs and tracked products after a fault. Many integration problems appear during these transitions rather than steady running.
Treat inspection and packaging quality as speed constraints
Increasing throughput can shorten camera exposure opportunities, reduce sealing contact time, or leave less distance for a reject mechanism to act. The quality system belongs in the timing budget, not in a later accessory specification.
For vision inspection, check motion blur, illumination, processing time, trigger repeatability, and result association with the correct pack. For rejection, confirm the mechanism’s response, consecutive-reject capability, and reject verification. A system that identifies a defective pack but removes its neighbor has not met the requirement.
Speed must also remain subordinate to validated process conditions and safety requirements. Faster operation may change stopping distances, guarding needs, or product handling risks. Review these against the machine design and destination-market requirements; faster controls alone do not establish safe operation.
Make supplier demonstrations prove the operating envelope
A peak-speed video is weak evidence for a line investment. Agree on factory and site acceptance criteria before ordering, using representative products and packaging materials. Record good output, rejects, stops, and interventions separately so a high running rate cannot conceal poor operating performance.
- Run representative and difficult formats long enough to reveal replenishment needs and thermal effects.
- Introduce agreed upstream starvation and downstream blockage, then examine restart behavior and buffer recovery.
- Test inspection and rejection at the specified maximum operating rate with controlled defect samples.
- Measure changeover through stable, acceptable production—not merely completion of mechanical adjustments.
- Verify fault diagnosis, recipe restoration, software backups, and operator recovery procedures.
Require time-stamped event records and clear definitions of downtime. The purpose is to distinguish inadequate machine capacity from poor coordination, material variation, or a test setup that does not represent production.
Include delivery and maintainability in the final decision
Industrial automation systems for packaging also depend on support after commissioning. Compare replacement-drive availability, controller lifecycle status, engineering-software access, local service coverage, and responsibility for interfaces between vendors. A technically capable line can remain unavailable if a failed component or inaccessible program prevents recovery.
For cross-border sourcing, confirm destination electrical requirements, documentation languages, applicable conformity obligations, and spare-parts logistics. Global Trade Insights & Industry Network (GTIIN) provides structured industrial and trade information that can help procurement teams place supplier capabilities and regional supply risks in context. That information complements, rather than replaces, machine-specific engineering evidence.
Before approving a proposal, assemble one agreed requirement sheet covering format-specific output, timing tolerances, buffer behavior, quality limits, recovery sequences, and acceptance tests. Select the system that demonstrates those conditions with maintainable hardware and clear integration ownership—not the one with the largest throughput figure on its brochure.
 How to use supplier risk analysis to spot financial warning signsUse supplier risk analysis to spot cash flow pressure, debt risks, and delivery warning signs. Learn practical steps to reduce exposure and protect supply continuity.
 When dual sourcing makes sense in a sourcing strategy for manufacturersSourcing strategy for manufacturers: learn when dual sourcing strengthens supply continuity, reduces disruption risk, and protects production without adding unnecessary complexity.
 How bulk commodities pricing affects long-term supply contractsBulk commodities pricing shapes long-term supply contracts through index rules, freight, quality, volume, and currency risk. Explore strategies for resilient costs and supply security.
 Which global manufacturing trends by sector matter most for sourcing plans?Global manufacturing trends by sector: identify sourcing risks, supplier resilience, compliance demands, and cost drivers to build smarter, more reliable procurement plans.
 What industrial trade intelligence pricing should include before you subscribeIndustrial trade intelligence pricing explained: compare coverage, data quality, access rights, and workflow value before choosing a subscription that supports smarter trade decisions.
 How an industrial trade intelligence dashboard can identify new supplier marketsDiscover how an industrial trade intelligence dashboard helps identify new supplier markets by comparing capacity, landed cost, logistics resilience, and compliance risk.
 Which global market entry barriers should exporters assess first?Global market entry barriers exporters should assess first: tariffs, compliance, buyer qualification, logistics, and payment risk. Build a practical strategy for confident market entry.
 How trade data aggregation analytics can reveal emerging supplier marketsTrade data aggregation analytics reveals emerging supplier markets by connecting trade flows, capacity signals, logistics, and compliance insights for smarter sourcing decisions.
 When an export market analysis platform can validate demand in a new marketExport market analysis platform insights help validate new-market demand through buyer fit, regulations, logistics, competition, and profitable entry conditions.
 What is driving the beauty and personal care market in the USA?Beauty and personal care in USA is driven by targeted solutions, selective premiumization, digital discovery, clean-label trust, diverse needs, and compliance. Explore key growth opportunities.
 How trade flow monitoring reports reveal changing regional demandTrade flow monitoring reports reveal changing regional demand through import volumes, sourcing shifts, product mix, logistics signals, and regulatory trends. Explore actionable market insights.
 How international market intelligence for investors reduces market-entry riskInternational market intelligence for investors reduces market-entry risk by validating demand, regulations, logistics, and competition before capital is committed.
 How international sourcing intelligence helps identify supplier risk earlyInternational sourcing intelligence helps businesses spot supplier risks early, protect supply continuity, and make smarter global procurement decisions.
 How trade data aggregation analytics reveals emerging supplier marketsTrade data aggregation analytics reveals emerging supplier markets through export trends, input flows, logistics, and regulatory signals. Discover smarter sourcing insights.
 What industrial cluster monitoring in Vietnam reveals about site riskIndustrial cluster monitoring Vietnam reveals hidden site risks across labor, utilities, logistics, compliance, and supplier dependencies. Make smarter sourcing and expansion decisions.
 Food Technology Trends Reshaping Shelf Life, Safety, and Product InnovationFood technology is reshaping shelf life, safety, and innovation. Discover the trends helping food businesses cut risk, improve compliance, and unlock stronger global market growth.
 How electronics manufacturing services are changing with low-volume demandElectronics manufacturing services are evolving fast with low-volume demand. Learn how agile EMS partners improve flexibility, compliance, sourcing resilience, and speed to market.
 How Can Buyers Reduce Procurement Risks for Electronic Components?How to reduce procurement risks for electronic components: learn how buyers assess traceability, lead times, compliance, and supplier types to avoid costly sourcing mistakes.
 What Sourcing Intelligence India Reveals About Supplier Risk and Cost ShiftsSourcing intelligence India reveals hidden supplier risk, compliance gaps, logistics pressure, and real cost shifts—helping buyers compare vendors smarter and source with more confidence.
 Fashion Trends 2026: Which Materials, Colors, and Silhouettes Are Gaining Ground?Fashion trends 2026 spotlight tactile fabrics, mineral colors, and controlled volume. Explore the materials, shades, and silhouettes shaping smarter, more wearable style.
 Smart Device Market Outlook: Key Growth Drivers, Segments, and Business OpportunitiesSmart device market trends are shifting toward system value, industrial demand, and resilient supply chains. Explore key growth drivers, high-potential segments, and business opportunities.
Global Trade Insights & Industry
Our mission is to empower global exporters and importers with data-driven insights that foster strategic growth.
Search News
Popular Tags
Industry Overview
The global commercial kitchen equipment market is projected to reach $112 billion by 2027. Driven by urbanization, the rise of e-commerce food delivery, and strict hygiene regulations.